


3-Ton Premium Tube Ice Machine System
Project Overview
This case study showcases a highly compact and intelligent 3-ton daily capacity tube ice machine system engineered by Kendall Group for a premium ice manufacturing and high-end hospitality beverage supply chain. The client distributes ice to elite hotel networks, bars, and food retail franchises that demand flawlessly clear, uniform, hollow cylindrical tube ice matching top-tier food-grade safety standards.
Their previous multi-unit modular setups were hindered by erratic ice cutting thickness, complex decentralized wiring that made troubleshooting a nightmare, and an open layout vulnerable to external airborne contamination.
Client Pain Points & Project Requirements
Core Pain Points
Microbial Risks & Hard-to-Clean Systems: Conventional open-frame designs allowed dust accumulation, while poor piping layouts made routine sanitation and chemical flushing highly inefficient.
Complex Maintenance & Wiring Chaos: Legacy equipment lacked centralized smart diagnostics, meaning a single sensor failure could halt the entire line while technicians spent hours tracing unlabelled wires.
Inconsistent Sizing & Mechanical Waste: Inefficient ice cutting mechanisms often generated excessive crushed snow/shavings waste, reducing the yield of premium sellable tube ice.
Customized Project Requirements
Sanitary Closed-Loop Operation: Full food-grade compliance with all water-contact components built from non-corrosive materials.
Smart "Turnkey" Automation: A centralized control hub supporting self-diagnostics and automated cycles from water filling to ice harvesting.
Ultra-Compact Footprint: A single, unified skid design capable of moving effortlessly through standard industrial doors and operating in space-restricted urban hubs.
The Kendall Tailored Solution
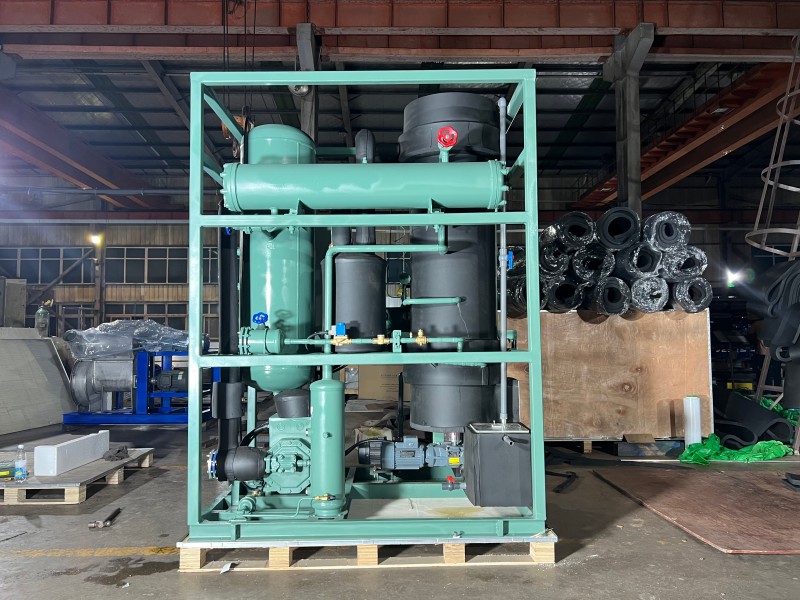
Kendall delivered a masterfully integrated, skid-mounted 3-ton tube ice solution. Every component is engineered to deliver pristine commercial ice within an ultra-reliable, self-contained architecture.
1. Intelligent Automated Control Hub (PLC Management)
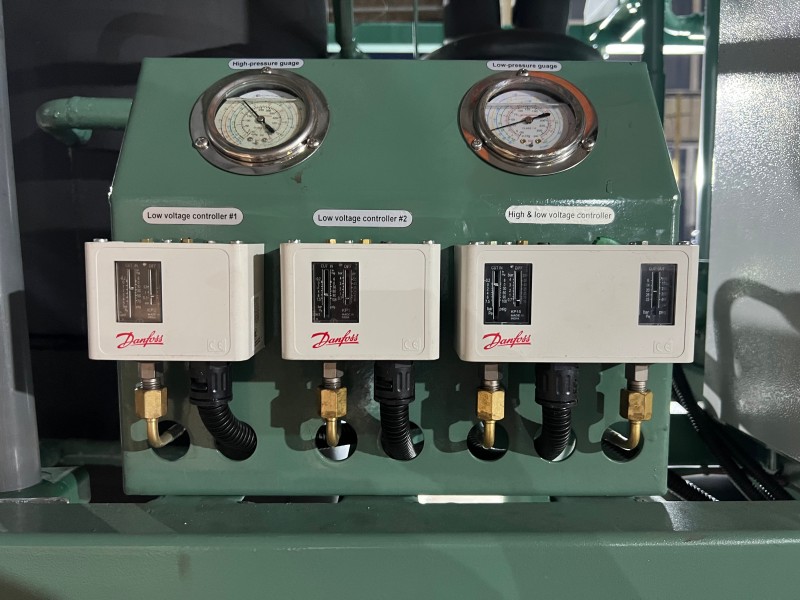
A standout feature of this unit is its premium, front-facing intelligent electrical control cabinet. Engineered with a clean, logically channeled wiring matrix, it integrates a smart PLC control system and dedicated circuit protection. The system runs fully autonomous cycles—managing precision water dosing, freezing intervals, hot-gas defrosting, and ice-cutting. Real-time diagnostic data allows operators to monitor performance instantly, making operation virtually foolproof.
2. Premium Core Compressor: Heavy-Duty Bitzer System
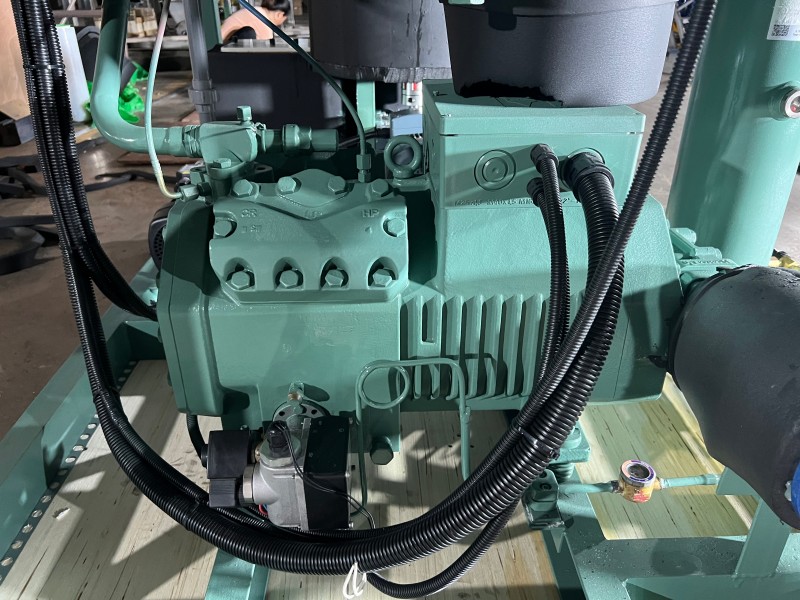
Positioned securely in the lower right chassis, the unit is driven by a genuine, highly efficient Bitzer semi-hermetic compressor. Specially selected for commercial tube ice production, it provides excellent compression ratios and high energy efficiency even under demanding ambient conditions. Its vibration-dampened installation guarantees quiet workshop operation and a prolonged equipment lifespan.
3. Advanced Vertical Tube Evaporator & Optimized Hydraulics
On the left stands the high-efficiency vertical tube ice evaporator, completely sealed in a high-grade, black thermal insulation jacket to eliminate cooling losses. Paired with a heavy-duty, stainless steel water circulation pump at the base, water is distributed smoothly down the internal freezing tubes. This constant, controlled film movement ensures the resulting tube ice is crystal clear, free of air bubbles, and perfectly formed.
4. Rigid Skid-Mounted "Plug-and-Play" Framework
The entire assembly—including the evaporator, Bitzer compressor, liquid receiver tank, and control cabinet—is built into a heavy-duty, green-coated structural steel cage. As shown sitting ready on its shipping pallet, this fully pre-piped and pre-wired design eliminates complex on-site construction. The client simply hooks up water and power to begin high-efficiency ice production immediately.


