


20-Ton Industrial Direct-Evaporation Block Ice Plant
Project Overview
This case study highlights a heavy-duty 20-ton daily capacity industrial block ice plant engineered and deployed by Kendall Group for a major maritime fishing port and cross-regional agricultural logistics hub. The facility requires a massive, continuous supply of large, slow-melting ice blocks to preserve massive seafood catches directly at the quay and sustain freshness during multi-day overland transport.
The client's previous legacy system relied on an outdated brine (saltwater) tank design. This traditional infrastructure was plagued by severe chemical corrosion, extended freezing cycles exceeding 24 hours, and grueling, hazardous manual ice harvesting that chronically bottlenecked port operations during peak fishing seasons.
Client Pain Points & Project Requirements
Core Pain Points
Severe Brine Corrosion & Maintenance Costs: Traditional calcium chloride saltwater tanks led to rapid chemical rust on the crane systems and surrounding machinery, driving up structural maintenance overhead and creating physical contamination risks for the ice.
Sluggish Thermal Exchange: The indirect heat transfer of salt water resulted in slow freezing cycles, making it impossible to keep pace with rapid fishing vessel turnaround times during peak seasons.
Intensive & Hazardous Manual Harvesting: Dragging, lifting, and thawing heavy ice blocks out of saltwater tanks required high manual labor, posing continuous safety risks to operators and slowing down outbound logistics.
Customized Project Requirements
Direct-Evaporation Eco-Technology: 100% elimination of traditional brine tanks to completely stop corrosion and guarantee pure, pristine, food-grade ice blocks.
Accelerated Freezing & Yield Stability: High-efficiency heat transfer infrastructure to significantly shorten the freezing cycle and secure a guaranteed daily output of 20 tons.
Mechanized Auto-Tipping & Delivery: Fully integrated mechanical or hydraulic lifting and tilting systems to automate block discharge directly to the loading dock with minimal manual intervention
The Kendall Tailored Solution
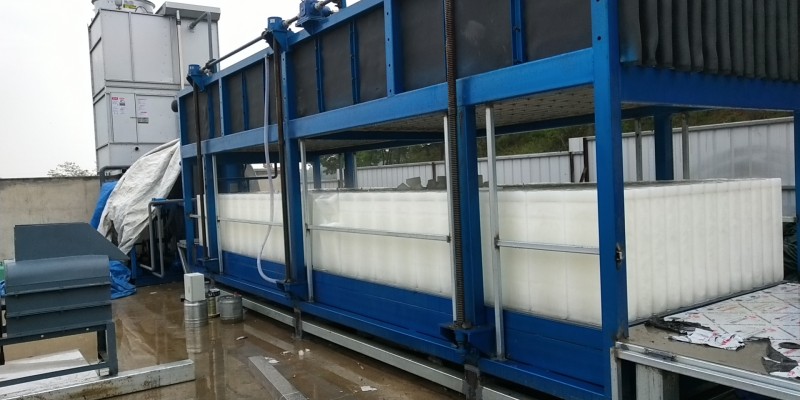
Kendall delivered a state-of-the-art, direct-evaporation block ice plant. Built within a rigid, integrated structural steel chassis, the system combines massive thermal capacity with modern automated logistics.
1. High-Efficiency Direct Evaporation Aluminum Alloy Technology
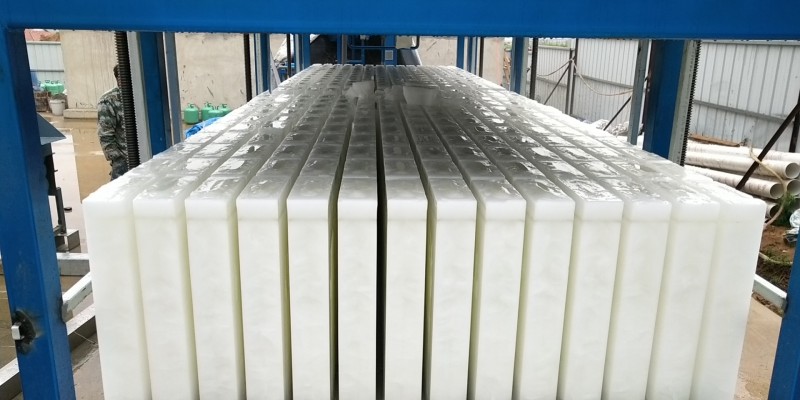
Kendall completely replaced the corrosive brine tank with premium-grade, certified aluminum alloy extrusions as the direct-evaporation ice molds. The refrigerant flows directly inside the internal channels of the aluminum walls, maximizing heat transfer. This cutting-edge engineering shortens the freezing cycle by over 30%, drastically lowering energy consumption per ton of ice and eliminating saltwater pollution entirely.
2. Mechanized Automated Ice Harvesting
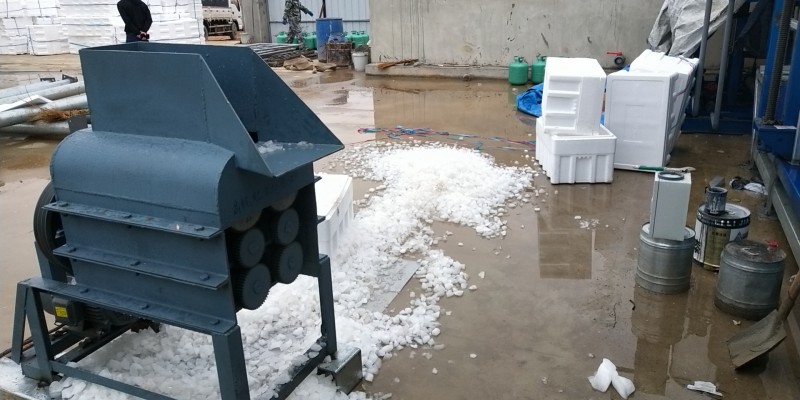
The plant integrates a synchronized mechanical lifting and automated tipping framework. Once the freezing cycle is complete, the smart system initiates an automated hot-gas defrost cycle to seamlessly release the ice blocks from the aluminum walls. The integrated mechanical grid then automatically lifts and tilts the blocks, sliding them directly toward the conveyor or crushing station, completely freeing workers from heavy physical labor.
3. Industrial-Grade Continuous Reliability & Closed Cooling Integration
The entire infrastructure is housed within a heavy-duty, protective blue structural steel cage designed to withstand harsh maritime environments and high-humidity tropical climates. Paired with a high-capacity industrial closed-circuit cooling tower (visible in the background), the system maintains optimal condensing pressures even under extreme ambient heat, ensuring uninterrupted 24/7 high-load operations.
4. Turnkey Lifecycle Engineering & Seamless Commissioning
Upholding Kendall's rigorous engineering standards, our project division managed the entire lifecycle of the plant—from the custom structural design matching the client's concrete dock site to precision piping installation, cooling tower balancing, and electrical commissioning. Following hand-off, comprehensive operational training was provided, backed by our global proactive after-sales framework to ensure long-term, high-efficiency investment returns.


